Why Factory Acceptance Testing Matters
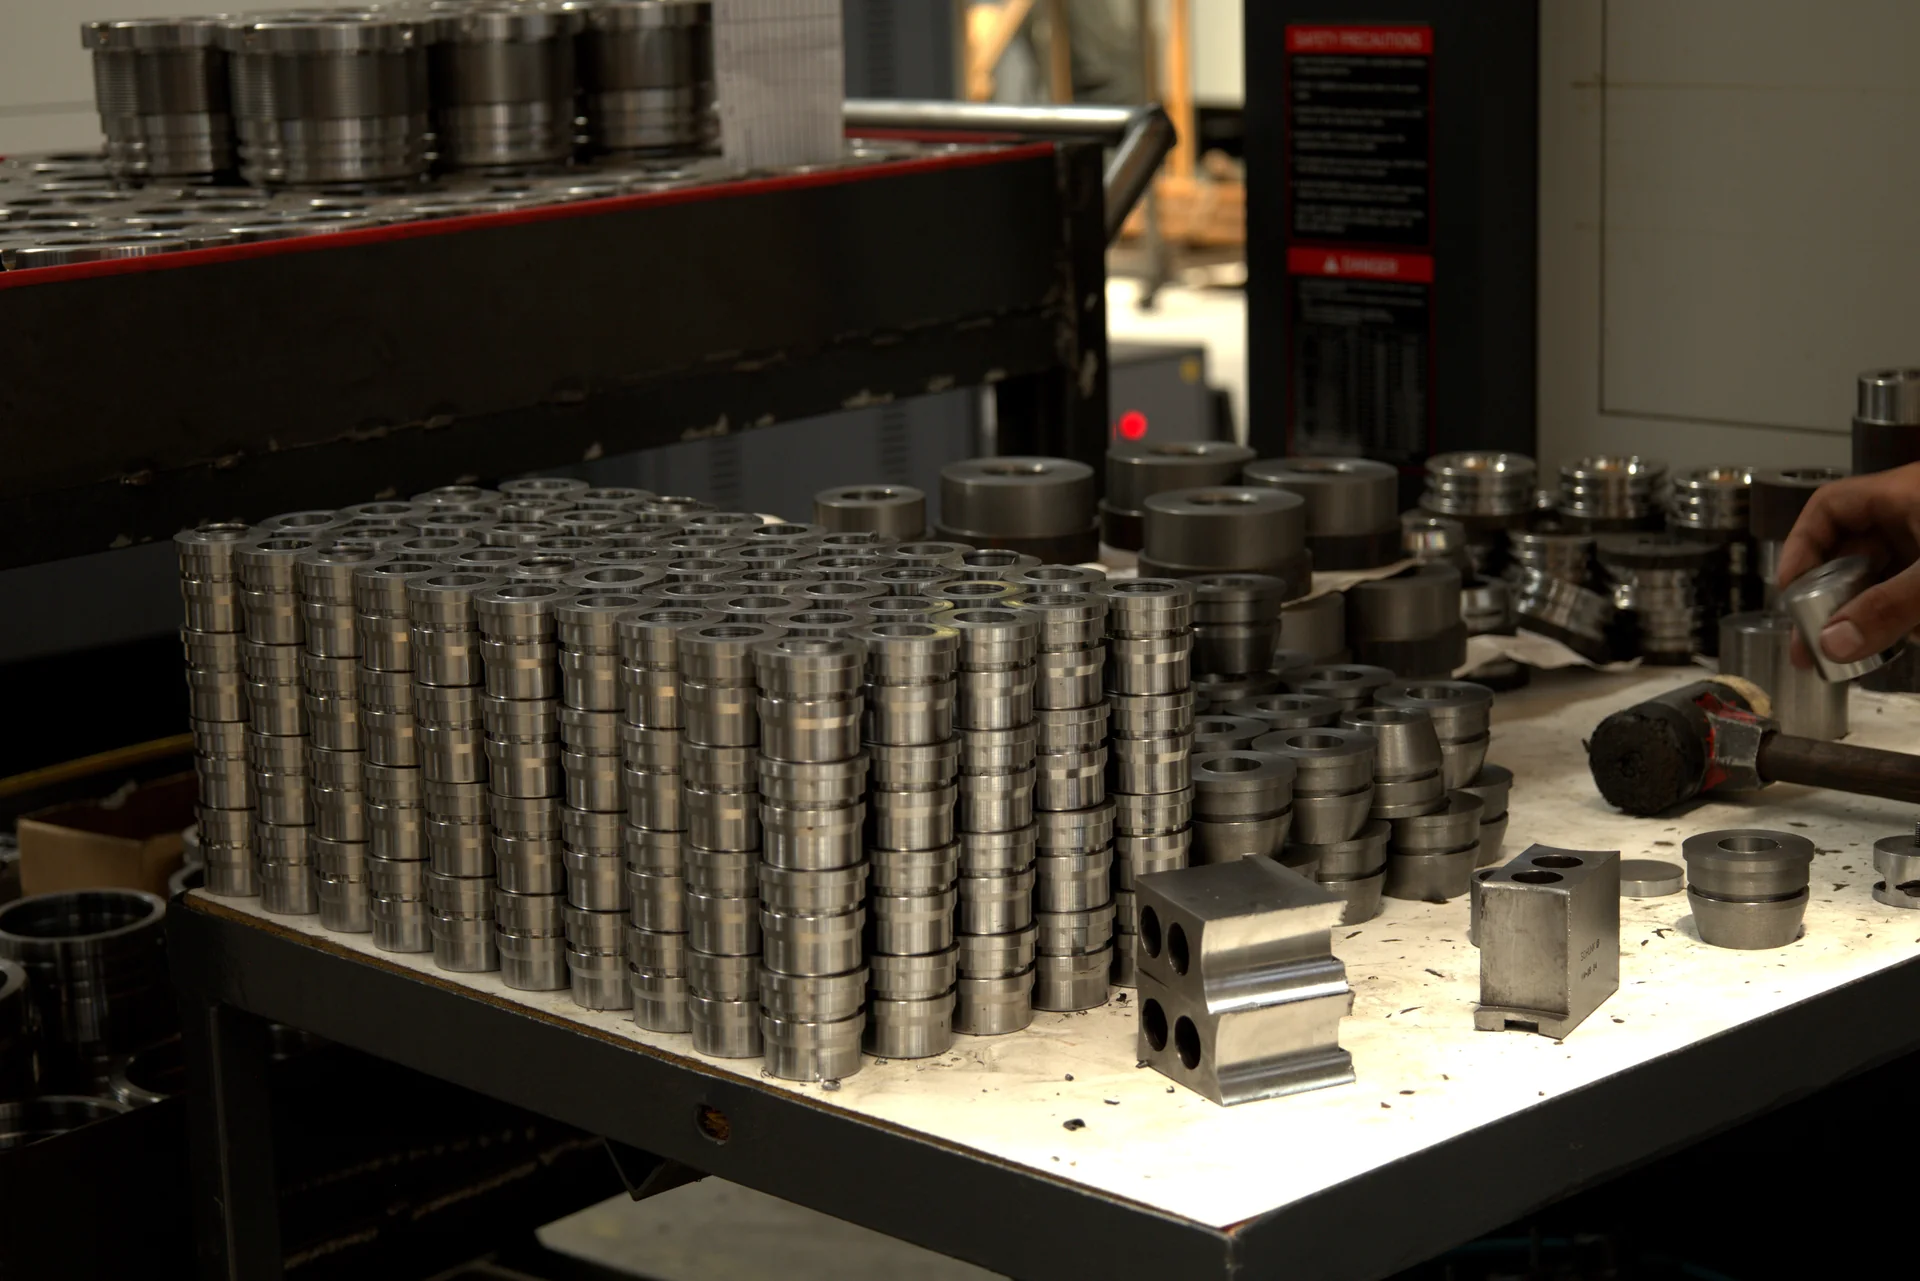
A hydraulic cylinder is a pressure-containing component, and a defect that escapes the factory becomes a field failure. Factory acceptance testing verifies each individual cylinder, not just the design or a sample. It detects assembly errors, seal damage and porosity before the cylinder is installed in a machine. At HPS, machining, welding, assembly and testing are all performed in-house on the 20,000 m² site in Konya/Karatay, so test results feed directly back into production. For buyers exporting equipment, a documented test is also the basis for traceable quality records.
ISO 10100 and Testing up to 1.5x Rated Pressure
ISO 10100 defines the acceptance test for hydraulic fluid power cylinders. HPS tests every cylinder to this standard at up to 1.5 times its rated working pressure. HPS cylinders are rated for working pressures of 200 to 250 bar; at a 250 bar rating the test pressure is therefore up to 375 bar. The overpressure margin proves that the tube, welds, rod, and static and dynamic seals withstand loads above anything expected in normal service. System-level safety remains governed by ISO 4413, and fatigue behaviour is addressed separately under ISO 10771-1.
Test Bench Procedure, Step by Step
The test runs on a dedicated test bench in a fixed sequence. First, the cylinder is cycled over its full stroke to confirm smooth motion, correct stroke length and correct port function. Second, an internal leak check verifies that pressurized fluid does not bypass the piston from one chamber to the other. Third, an external leak check inspects the rod seal, port connections and welds for any visible leakage at test pressure. Finally, a drift (holding) check pressurizes the cylinder in a fixed position and monitors rod movement over time; measurable drift indicates internal bypass. Only cylinders that pass all steps are released for shipment.
What Internal Leakage Means: Piston Seal Bypass
Internal leakage is fluid passing from the high-pressure chamber to the low-pressure chamber across the piston seal, known as piston seal bypass. The cylinder can still move, so the defect is invisible from outside, but the load creeps under pressure and holding capability is lost. On the test bench it is detected as rod drift while the cylinder is held pressurized in a fixed position. The pass criteria concept is simple: drift and leakage must stay within the acceptance limits defined for the test before a cylinder is approved. Seal material also matters: HPS fits NBR as standard up to about 90 C, with HNBR, PU, FKM and PTFE options, and final seal selection is verified by engineering.
Documentation: Pressure Test Report and EN 10204 3.1
A pressure test report is issued on request for every accepted cylinder. For material traceability, EN 10204 3.1 material certificates are available on request for pressure-carrying components such as the tube and rod. Typical documented materials are DIN 2391-2 ST52 / EN 10305-1 E355 tube and CK45 or 42CrMo4 rod. These documents let quality departments link each cylinder to its test result and its material documentation. HPS exports to 49 countries under HS code 8412.21, with EXW, FCA, CIP, CIF and DAP Incoterms; the certificates travel with the commercial documentation.
Related Verification: Rod Chrome Layer and H8-H9 Honing Tolerance
Pressure testing is the final gate, but two upstream verifications determine long-term sealing performance. The piston rod is CK45 or 42CrMo4 with a hard-chrome layer of about 30 µm (min. 20 µm); it arrives as certified bar with an EN 10204 3.1 certificate and is checked at incoming inspection. The cylinder tube is supplied honed to an H8-H9 tolerance, giving the bore the geometry and surface finish the piston seal needs to seal reliably. Rod coating quality and bore tolerance directly influence external leakage at the rod seal and internal bypass at the piston. Full technical parameters, including live force and buckling calculations, are available in the online configurator on the HPS website.
- How to Size a Hydraulic Cylinder: Bore, Rod, Stroke and Pressure →
- Euler Buckling in Hydraulic Cylinders: When Long Stroke Drives the Design →
- Telescopic Cylinder Staging: How Multi-Stage Hydraulic Cylinders Are Designed →
- Single-Acting vs Double-Acting vs Telescopic Cylinders: Selection Guide →
- Hydraulic Cylinder Troubleshooting: Drift, External Leakage, Noise and Slow Operation →